Huismerk vs OEM vs ODM waterpijp: welk model past bij jouw merk?
October 3, 2026
Custom Logo Methods for Hookah: Laser, Engraving & Printed Options
October 3, 2026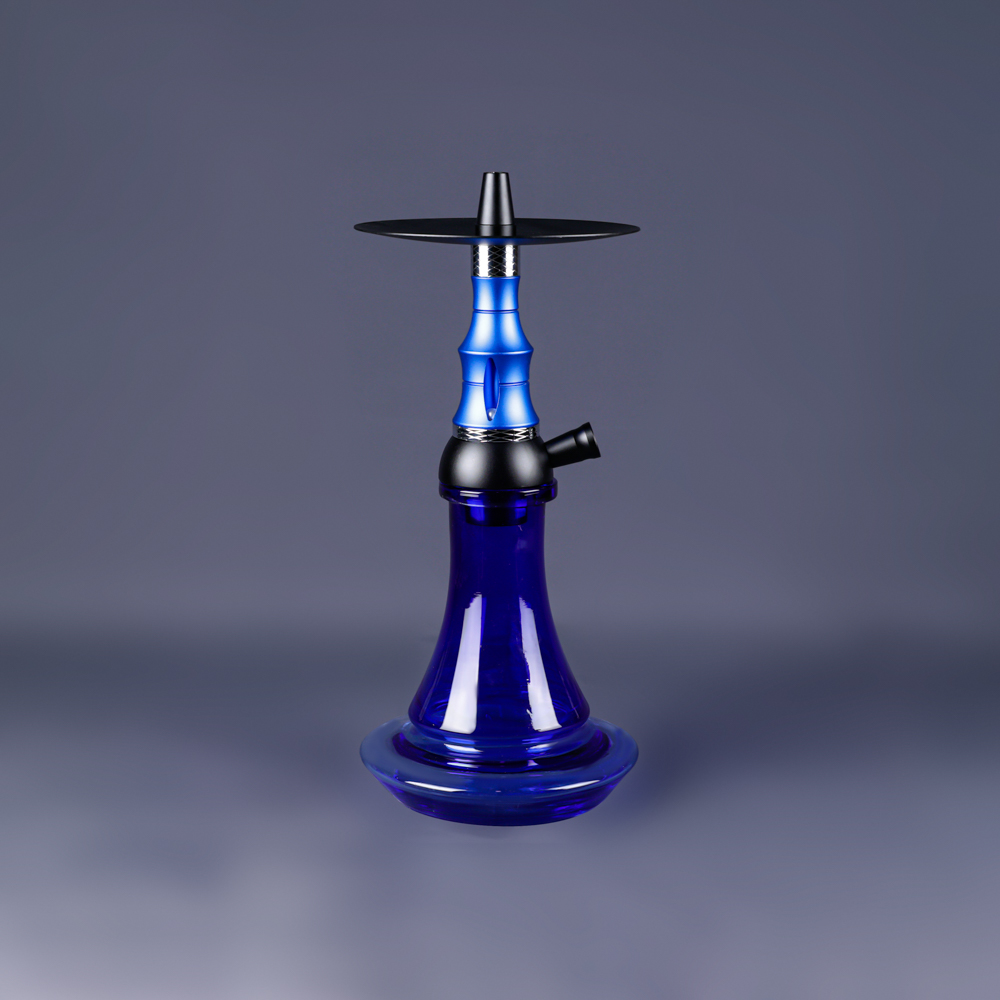
Hookah Finish Options: The Short Answer Up Front
Hookah finish options decide how a unit feels in the hand, how it photographs online, how it survives a lounge floor, and how many complaints reach you months after delivery. The finish is what your customer sees first and complains about last.
This guide compares the five finishes that cover most wholesale programs — electroplating, matte paint, PVD coating, anodized aluminium, and brushed or sandblasted metal — then covers the biggest after-sales headache: fading and peeling.
The short version: plating buys luxury, matte paint buys color freedom, PVD buys hardness, anodizing is the durable default for aluminium, and brushed or sandblasted finishes buy hand feel and fingerprint resistance.
| Finish | Relative cost | Wear resistance | Fade resistance | Color range | Compliance notes | Best-fit tier |
|---|---|---|---|---|---|---|
| Electroplating (chrome, gold) | Low to mid | Moderate; chips first at edges | Moderate; gold can dull | Metallic tones only | Hexavalent chrome under pressure | Mid to high-end retail |
| Matte paint | Low to mid | Low to moderate; edge chips | Good if quality high; UV risk | Very wide, incl. custom | Solvent/VOC controls | Entry to mid |
| PVD coating | High | Very high | Very high | Moderate to wide | Vacuum; low emissions | Premium and flagship |
| Anodized aluminium | Mid | High on aluminium | Very high; dye sealed in oxide | Wide | Acid and wastewater treatment | Mid to premium aluminium |
| Brushed / sandblasted | Low | High; base metal wears evenly | No color film | Neutral metal tones | Mechanical; minimal chemistry | All tiers |
Read the table as a map, not a ranking. A cheap finish applied properly beats an expensive finish applied badly.
Electroplating: Chrome, Gold, and Rose Gold Plating
Electroplating deposits a thin metal layer — chromium for mirror-bright silver, gold or rose gold for warmth — onto a polished substrate, usually brass or zinc alloy. It is fast, widely available, and delivers the highest gloss per cost of any finish.
- Instant perceived value. High-polish chrome or gold reads as luxury in a photo and on a shelf.
- Gold sells in traditional markets. Warm gold tones drive demand in the Gulf, not just complete a spec.
- Low entry cost and a mature supply base. Plating shops are everywhere, so sourcing is rarely a bottleneck.
- Adhesion depends on the substrate. Polishing residue, casting porosity, or an uneven base produces flaking.
- Edges and threads are thin. Coverage drops where the part is handled most, so those points fail first.
- A chip becomes a corrosion point. Once the film breaks, the base metal is exposed and damage spreads.
- Chrome faces regulatory pressure. Traditional hard chrome often uses hexavalent chromium, regulated in the EU and increasingly elsewhere; trivalent substitutes must be requested. Confirm the current position with official sources.
Plating performs well only when substrate prep is disciplined; heavy shared use exposes the edges.
Matte Paint: Color Freedom with Limited Scratch Resistance
A matte hookah finish is the fastest route to a modern look. Painted finishes — liquid or powder — take color easily, making them the natural choice for a signature color, a limited edition, or a coordinated range.
- The widest color range of any finish, including custom brand colors and coordinated multi-part ranges.
- A contemporary aesthetic. Matte black, gunmetal, and muted tones photograph cleanly and suit minimal branding.
- Cheaper color changes than PVD or anodizing.
- Paint is a film, and films chip. Base rims, threads, and ports wear through — the most common source of peeling complaints.
- Scratches are permanent. Matte hides fingerprints better than gloss, but a scratch in the film cannot be buffed out.
- Prep and cure decide everything. Primer is essential; under-cured paint fails in the field even if it passed a rough factory check.
If you sell painted hookahs into lounges, expect edge wear; powder coating is tougher than liquid paint for high-abuse parts.
PVD Coating: Hardness That Justifies the Premium
PVD coating on a hookah — Physical Vapor Deposition — deposits a very thin metallic or ceramic film in a vacuum chamber. The result is hardness well beyond plating, in gold, black, champagne, rose gold, and specialty tones that hold their color far longer.
- Hardness and scratch resistance. The film resists daily abrasion that would dull plating, so a premium claim survives real use.
- Color durability. Color comes from the film’s composition, not a dye, so it does not fade like cheap paint.
- Higher unit cost. Batch vacuum processing puts PVD at the top of the cost ladder — typically several times a simple plating cost, depending on geometry and order size.
- Longer lead times. Batch vacuum cycles add scheduling risk, especially for rush orders.
PVD belongs on flagship SKUs and gift sets, where the finish is part of what the customer pays for.
Anodized Aluminium: The Workhorse for Aluminium Parts
Anodized hookah parts are the default for good reason. Anodizing grows a hard oxide layer on aluminium and seals dye into it. Unlike paint or plating, it is not a film on top — it is part of the metal, which is why it does not peel or flake.
- Excellent fade resistance. Sealed dye holds color far better than paint, and handling does not wear it away.
- Good wear resistance. The oxide layer stands up to regular use on a bar top or lounge table.
- Broad color range, no flaking failure mode. Black, gold, red, blue, and gunmetal are achievable, and anodized color does not chip off in sheets.
- Aluminium only, so it does not apply to brass or stainless steel.
- Batch-to-batch color variation. Dye lots can shift tone, so approve a golden sample and hold suppliers to it.
- Bright dyes fade faster under strong UV, and aluminium dents more easily than brass.
For aluminium stems, inner tubes, and accessories, anodizing is usually the best balance of durability, color, and cost.
Brushed and Sandblasted: Texture, Hand Feel, and Fingerprints
Brushed and sandblasted finishes are mechanical, and they are often the base step for another finish. A good blast improves adhesion for plating, paint, and anodizing, which is why prep quality and finish quality travel together.
- Brushed creates a directional grain that gives a premium, industrial look and hides light scratches.
- Sandblasted produces a uniform matte with a soft hand feel that resists fingerprints and disguises minor scuffs.
The cautions are minor: texture can trap residue, blast coverage can be uneven, and grain direction must be consistent. As a base prep, blast quality is one of the cheapest levers over finish durability.
The Biggest Complaint: Fading and Peeling
If one issue drives returns in this category, it is color fading and paint or plating peeling off. Most root causes are preventable at the factory, before the container ships.
- Inadequate substrate preparation. The number-one cause. Oil, polishing residue, oxidation, or a rough casting stops the finish from bonding.
- Uneven film thickness. Plating and paint thin out at edges, threads, and sharp contours — the high-wear points, so they fail first.
- Wrong finish for the environment. A decorative finish pushed into hot, humid, or heavily handled service wears out early; match the finish to the duty, not the look.
- Weak process discipline. Under-cured paint, contaminated baths, worn anodes, or insufficient dye sealing all produce early failure.
- Cheap dyes and transit damage. Low-grade dyes fade faster under light; parts rubbing in packaging chip at edges before use.
How to cut complaints before they happen:
- Specify prep and finish in writing — substrate preparation, process, color, and gloss level, not just “gold” or “black.”
- Require a production-representative sample, since a hand-finished sample can outperform mass production. Define the acceptance test in advance.
- Protect high-wear points with a metal or anodized collar instead of paint at threads and rims.
- Keep a golden sample for every SKU and color, and compare future batches against it.
- Pass on care instructions, since most premature damage comes from the wrong cleaning method.
Testing Adhesion: Simple Checks Before You Commit
You do not need a laboratory to catch most finish problems. These checks run on a sample at your desk or during a factory visit.
- Tape test (cross-hatch adhesion). Score a grid of cuts through the finish, press standard adhesive tape over it, and pull. Finish coming away points to poor adhesion. This mirrors the recognised cross-cut tests (ASTM D3359 and ISO 2409) — if a supplier cites one, ask to see the report and confirm the current edition with the standards body.
- Fingernail and coin scratch test. Drag a fingernail or coin edge across a low-visibility area. Plating, paint, and PVD should resist normal handling force; anything that lifts instantly is too soft for service.
- Edge and thread inspection under light. A loupe on the thinnest coverage points — edges, threads, ports — exposes dull patches, bubbles, pinholes, exposed base metal, orange peel, and inconsistent grain.
- Third-party salt spray testing. For large programs, ask for accelerated corrosion testing (such as ISO 9227 salt spray) from an accredited lab, and confirm it covers your exact finish and substrate.
Market Aesthetics and the Cost of a Finish Upgrade
Finish preference is regional, and matching it is often worth more than a marginal price advantage.
- Middle East (Saudi Arabia, UAE, the Gulf). Gold, high-polish chrome, and brass tones dominate; ornate, high-gloss plating signals ceremony, so gold plating and gold-tone PVD both sell.
- United States. Matte black, gunmetal, and anodized aluminium lead; lounges lean toward durable, hygienic designs.
- Europe (Germany, France, the Netherlands, Poland). Understated matte and black aluminium are favored, and buyers screen finishes on environmental grounds, so trivalent chrome and documented wastewater treatment carry weight.
- Russia and nearby markets. Accessible prices matter most, with gloss chrome and gold still in demand.
What Finish Does to Your Quote and Lead Time
- Setup cost per color. Small MOQs per color spread that cost over fewer units, so splitting an order across colors raises the effective price.
- Process steps and rejects. PVD and anodizing add steps and a measurable reject rate, both feeding unit price.
- Extra lead time. Finishing adds process and curing time, and PVD adds batch vacuum cycles. Custom colors usually need sampling rounds before mass production — days to weeks, so plan for it.
So when is it worth paying more? Pay when the finish is the selling point — a premium or gift SKU, or a market where gold and gloss drive the sale. Pay for better substrate prep before a fancier finish — the cheapest finish on a clean base beats a premium finish on a poor one. And skip premium finishes on parts nobody touches: internal tubes, hidden fittings, or consumables.
Choosing Among Hookah Finish Options: Procurement Checklist and FAQ
- Define the market, channel, and usage intensity. Retail or lounge, light or constant handling — that sets the durability bar before price.
- Choose the substrate first, then match the finish. Brass, stainless steel, zinc alloy, or aluminium — anodizing means aluminium.
- Specify prep, finish, color, and gloss in writing.
- Require a production-representative sample and third-party tests — adhesion and salt spray where the program warrants it.
- Confirm compliance for the destination market. Ask how your supplier handles chromium chemistry, VOCs, and anodizing wastewater, then verify current rules through official channels — the EU’s TARIC and REACH resources, or the US HTS database at hts.usitc.gov. Regulations change, so confirm the position yourself.
- Check MOQ per color, setup cost, and lead time, since the number of colors changes the effective unit price.
- Keep a golden sample and order packaging that protects the finish in transit.
Which hookah finish lasts the longest?
For aluminium parts, anodizing and PVD are the most durable in normal use — anodizing because the color is part of the metal, PVD because the film is hard and color-stable. On other substrates, PVD generally outlasts plating and paint. The bigger variable is application quality: any finish over a poorly prepared base fails early.
Why does gold plating peel off a hookah?
Almost always because of the surface underneath. Polishing residue, oxidation, or a porous casting stops the gold from bonding, and thin coverage at edges and threads fails first. Gold is also soft, so it scratches with heavy handling. If the gold look matters, ask about gold-tone PVD — it resists wear far better.
Is a matte finish durable enough for a hookah lounge?
It can be, if you accept edge wear. Powder coating is tougher than liquid paint. Keep painted surfaces away from the highest-wear points — threads, ports, and base rims — or switch those components to anodized or bare metal.
Do I need different finishes for the Middle East versus Europe and the US?
Yes, and it is one of the easiest ways to raise sell-through. Gulf buyers respond to gold and high-polish chrome; US and European buyers lean toward matte black, gunmetal, and anodized aluminium.
Finish is where appearance, durability, and landed cost meet, so it deserves more than one line in a quote. With 16 years of hookah manufacturing behind it, Hookah Omnis can quote electroplated, painted, PVD, anodized, and brushed options on the same design for side-by-side comparison — start with the wholesale hookah catalog or ask about ready-to-ship hookahs for a faster first order, then message us on WhatsApp with your market and target price. Our hookah wholesale FAQ answers the rest.